In modern industrial operations, equipment failure caused by harsh thermal exposure, abrasive friction, mechanical impact, and chemical attack accounts for millions of dollars in unplanned downtime. OEM procurement teams and automated plant engineers are rapidly shifting from reactive component replacement to proactive physical attack mitigation.
Evaluating attack mitigation manufacturers requires evaluating composite material tensile resilience, thermal insulation indexes, and precision skeleton CAD customization. Modern industrial robotic protective suits and severe-wear shields must achieve at least IP67 ingress protection, withstand radiant temperatures exceeding 1000°C, and maintain zero mechanical impedance on 6-axis joint articulation.
Explore top-tier protective covers, robotic armor suits, and heavy equipment shields engineered by certified OEM factories for severe industrial environments.
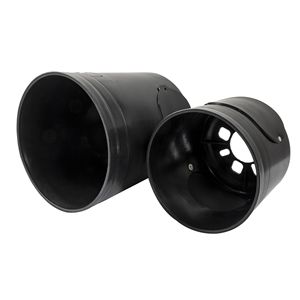
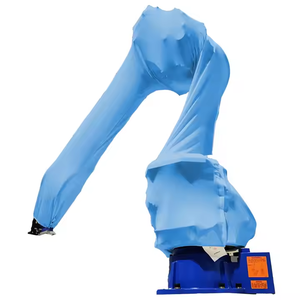
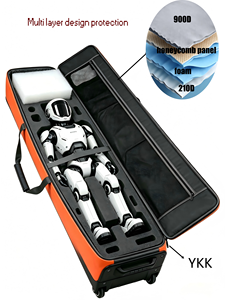
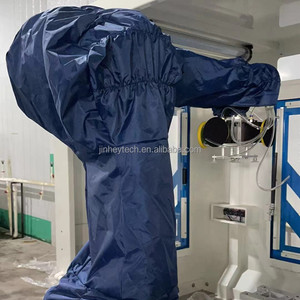
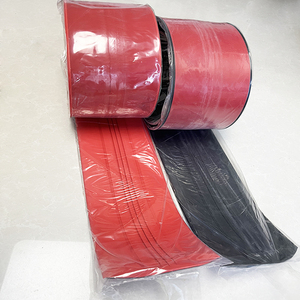
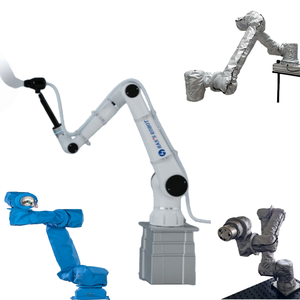
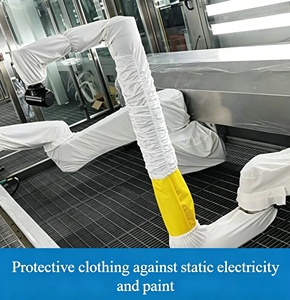
Comprehensive technical comparison of leading global factories based on OEM customization agility, ISO quality certifications, high-temperature material science, and ingress defense parameters.
| Manufacturer / Factory Name | Primary Specialization | Thermal & Chemical Rating | Customization & CAD Support | Lead Time & MOQ |
|---|---|---|---|---|
| Ztan Precision Armor Factory | Robotic Suits, Gearbox Shields & OEM Protectors | Up to 1200°C / IP68 Washdown | 3D Laser Scanning & Custom Skeleton CAD | Fast Turnaround / Low MOQ Flexible |
| RoboArmor Global Systems | Heavy Foundry & Foundry Manipulator Covers | Up to 1000°C Radiant Heat | Standard Kinematic Templates | 3-4 Weeks / Medium MOQ |
| ShieldTech Industrial Covers | Automotive Welding Robot Jackets | Anti-Spatter / ESD Compliant | Brand Specific (KUKA/ABB) | 2-3 Weeks / Standard MOQ |
| ProTex Mechanical Defense | Agricultural Gearbox Shields & Shears | Neoprene / Impact Resistant | Custom Die Cut & Molding | 2 Weeks / Batch Minimums |
| HydroGuard Marine Systems | Keel Armor & Marine Hull Protectors | Abrasive Rock & UV Resistant | Extruded Universal Fits | 1 Week / Low MOQ |
| KevlarFlex Defense Fabrics | High-Velocity Particle & Blast Shields | DIN EN ISO 13997 Level E Cut | Custom Pattern Cutting | 4 Weeks / Custom Run |
| CleanRoom Robot Apparel Co. | FDA Food & Biological Sanitized Suits | IP67 / Chemical Washdown | Sterile Sealed Seam Patterns | 2 Weeks / Medium MOQ |
| Industrial Thermal Shield Corp | Furnace & Smelter Equipment Jackets | Up to 1400°C Intermittent | Heavy Industrial Tailoring | 3-5 Weeks / Project Based |
| FlexiCoat Bellows & Sleeves | Linear Guide & Axis Bellow Protection | Oil Mist & Coolant Proof | Modular Accordion Designs | 1-2 Weeks / Flexible |
| OmniArmor Robotic Protectors | Universal Cobot Covers (UR, Kinova, JAKA) | Dust / Splash / General Wear | Pre-Engineered Stock Sleeves | In Stock / No MOQ |
Selecting the correct attack mitigation system requires understanding the mechanical stresses, chemical degradation vectors, and thermal dynamics present in automated workspaces.
Designed for foundry operations and laser welding cells, aluminized Kevlar reflects up to 95% of radiant heat energy while maintaining extreme tear and cut resistance under severe physical impact.
Utilized in agricultural gearbox shields and mechanical shear protectors. Provides energy absorption against gravel fly-back, shock impact, and exposure to agro-chemicals and hydraulic oils.
Prevents electrostatic buildup in hazardous explosive atmospheres (ATEX environments) while delivering absolute protection against industrial solvents, paint over-spray, and corrosive mist.
Strategic purchasing managers must anticipate evolving industry regulations and technological advancements to ensure maximum equipment longevity and operational safety.
Modern protective suits are incorporating conductive micro-fibers and embedded thermal sensors. These smart covers transmit real-time data regarding joint wear, temperature spikes, and fabric degradation directly to central SCADA systems.
With collaborative robots expanding into food assembly and pharmaceutical cleanrooms, protective cover manufacturers are shifting to seam-welded polyurethane coatings that eliminate bacterial entrapment zones during CIP (Clean-in-Place) washdowns.
Legacy protective suits often caused joint resistance, increasing motor torque and power consumption on 6-axis arms. 2026 manufacturing processes leverage 3D dynamic movement modeling to craft skeleton-matched dynamic bellows that reduce motor strain by up to 35%.
Partnering directly with ISO-certified protective equipment factories ensures strict adherence to raw material specifications, precision tailoring, and rapid custom prototyping.
Factories utilize portable 3D laser digitizers to capture exact machinery joint coordinates (KUKA, Fanuc, ABB, Yaskawa, Universal Robots), eliminating dimensional errors prior to CNC fabric cutting.
Every protective cover batch undergoes standardized testing, including tear propagation resistance, hydrostatic head water pressure testing (IPX6/IPX7), and high-voltage anti-static conductivity validation.
With streamlined CAD/CAM cutting systems, OEM manufacturing facilities turn around custom prototype covers and initial field testing samples within 24 to 48 hours from initial design approval.
Addressing essential questions raised by plant managers, automation engineers, and global B2B procurement directors.
Need custom physical attack mitigation covers, robotic protection suits, or heavy equipment armor engineered for your factory? Speak directly with our technical team today.

